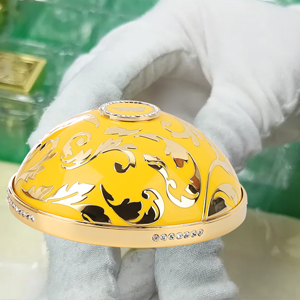
Hand-filled enamel perfume caps are among the most recognizable signatures of luxury fragrance packaging. The smooth, glass-like color, sharp clean lines, and jewelry-like finish create a premium look that printed or painted caps simply cannot match. But what most buyers don’t see is the intricate, multi-step production process behind every cap—one that combines precision metalworking with skilled handcraft.
As a professional enamel perfume cap manufacturer with 16+ years of specialized production experience, JSM has perfected a 7-stage manufacturing workflow that delivers consistent, defect-free enamel finishes at bulk scale. In this behind-the-scenes guide, we walk through every step of the process—from raw alloy to finished, shelf-ready cap—with real production parameters and quality controls.
You can also view our on-site factory photo walkthrough of the enamel production workflow on our process page.
1. Blank Preparation: Building the Zamac Foundation
Every enamel cap starts as a solid zamac (zinc alloy) blank formed through high-pressure die-casting. Zamak 3 alloy is the industry standard for enamel caps because of its excellent dimensional stability, smooth cast surface, and compatibility with low-temperature curing.
After casting, we perform three critical preparation steps:
- Gate removal & deburring: Sprue gates and casting flash are trimmed off, and all edges are ground smooth.
- Surface grinding: The entire blank is polished to create a uniform base surface.
- Recess sandblasting: The recessed grooves that will hold the enamel are bead-blasted to create a slightly rough, porous surface.
This sandblasting step is non-negotiable: it ensures the enamel glaze adheres firmly to the metal substrate, preventing glaze shrinkage, blistering, and peeling over the product’s lifecycle.
2. Enamel Glaze Preparation: Precision Formulation & Color Matching
Unlike paint, enamel is a glassy ceramic material that must be formulated to exact specifications. For zamac substrates, we use specialized low-temperature enamel powder rated for curing below 130°C—high enough to cure the enamel, but low enough to avoid melting or deforming the zinc alloy base.
The mixing process:
- Enamel powder is weighed out according to the batch size.
- AB glue resin is added at a strict 3:1 weight ratio (A:B) and stirred into a smooth, uniform paste.
- Color pigments are added to match the customer’s specified color standard.
Our color lab matches every batch to customer-provided PMS, RAL, or physical sample standards, with final color difference controlled to ΔE < 2.0—below the threshold of human visual detection. Standard color options include red, blue, green, black, white, and metallic enamel gold, but custom tones are available for volume orders.
3. Hand Enamel Filling (The Dotting Process)
Enamel filling is a skilled manual process that cannot be fully automated without sacrificing quality. Our trained technicians use fine needles, small spatulas, and precision syringes to deposit enamel paste into the recessed grooves, one color at a time.
Key quality rules during filling:
- Operators work under magnified lighting to ensure complete, even fill.
- Enamel is applied just below the rim of the groove to account for melt-level rise during firing.
- Overflow and color mixing are strictly avoided.
- For multi-color patterns, technicians wait until the previous color layer reaches semi-cure before applying the next to prevent bleeding between colors.
This handcraft step is what gives premium enamel caps their sharp, clean color lines—and it is also the biggest reason enamel caps carry a higher price point than standard plated caps.
4. High-Temperature Curing / Firing
After each color application, the caps are loaded into a controlled convection oven for curing.
Standard firing parameters:
- Oven temperature: approximately 110°C
- Curing time: 60 minutes
- Heating profile: gradual ramp-up to target temperature, then controlled hold
During firing, the enamel paste melts, levels out, and solidifies into a smooth, glossy, glass-like surface that is chemically bonded to the metal.
Complex multi-color designs require multiple rounds of filling → firing → cooling → next color. Intricate crests and multi-color logos can require 3–5 separate firing cycles to build the final design layer by layer.
5. Controlled Cooling & Deflashing
Cured caps undergo slow, controlled cooling (natural or gradual ramp-down) to prevent thermal shock, which would cause cracking, crazing, or enamel delamination.
Once fully cooled, our technicians perform post-firing finishing:
- Remove any enamel overflow and residual burrs by hand
- Inspect every cap under magnified light for missing enamel, pinholes, and air bubbles
- Perform spot repairs on minor defects, followed by secondary re-firing
Units with irreparable defects are rejected at this stage before moving on to final surface treatment.
→ Learn more about defect prevention in our guide to 10 common perfume cap quality issues and how we solve them.
6. Surface Polishing & Electroplating
After the enamel layer is finalized, the raised metal edges and surfaces are polished to a high-gloss finish. The cap then moves to electroplating, which serves three purposes:
- Seals the zamac base against corrosion and tarnish
- Enhances the visual depth of the enamel
- Creates a cohesive luxury finish across the entire cap
Available standard electroplating finishes include bright chrome, bright gold, matte gold, gunmetal, and rose gold—all customizable to brand specifications.
→ Explore every finish option in our complete guide to perfume cap electroplating finishes.
7. Final Inspection & Assembly
Every enamel cap passes through 100% final inspection before packaging, enforced under our ISO9001:2015 and SMETA certified quality management system.
Inspection criteria:
- Visual: Uniform color, no impurities, no chipped enamel, clean metal edges
- Tactile: Smooth surface, no sharp edges or scratchy points
- Functional: Proper fit with standard neck sizes and pump systems
Approved caps are then packed in foam trays to prevent scratching and damage in transit. For premium finishes, we offer individual PE bag wrapping at customer request.
Why This Process Makes Premium Enamel Caps Worth the Investment
Enamel caps cost more than standard plated zamac caps for good reason: the process is slower, more labor-intensive, and requires tighter process control. But the return on investment for premium brands is substantial:
- Unmatched color permanence: Enamel does not fade, scratch, or wear off like printing or paint.
- True premium differentiation: On a retail shelf, an enamel cap stands out immediately from generic metal closures.
- Long-term brand equity: Caps look brand new for years, protecting your product’s image on shelf and in use.
For mid-premium and luxury fragrance lines, enamel is one of the highest-ROI packaging upgrades you can make.
Frequently Asked Questions
Q: Why are enamel perfume caps more expensive than regular metal caps? A: Enamel requires additional raw materials, multiple extra production steps, and skilled manual labor for the dotting process. Multi-color designs also require multiple firing cycles. The result, however, is a significantly more premium product that supports higher retail pricing.
Q: How many colors can you do in one enamel cap? A: We regularly produce caps with 2–5 colors. More colors are possible but increase cost and lead time. Our engineering team will review your design and recommend the most cost-effective approach.
Q: Will enamel chip or peel off over time? A: When properly applied and cured, enamel is chemically bonded to the metal and will not peel or chip under normal use. It is significantly more durable than paint, printing, or labels.
Q: What is the lead time for custom enamel perfume caps? A: Standard production lead time is 30–40 days after sample approval, due to the multiple firing and inspection steps. Sampling takes 7–15 days for existing shapes. See our full custom perfume caps OEM guide for complete ordering details.
Q: Can you match our exact brand color? A: Yes. We can match PMS, RAL, or physical color samples. We always provide color drawdowns for approval before full production.
Premium Enamel Caps, Built to Your Brand
At JSM, every enamel cap is produced with the same level of precision and care, whether your order is 5,000 pieces for a limited edition or 50,000 pieces for a permanent SKU. Our in-house team controls every step of the process—from die-casting to final inspection—under one roof for consistent quality and lead times.
If you’re developing a custom enamel cap for your next fragrance launch, contact our engineering team today for a free design review, feasibility assessment, and detailed quotation.